Melting is not the same as extracting
Melting changes a solid into a liquid. It does not, by itself, separate silver from a mineral or make an alloy pure. That distinction matters whenever an image of molten metal is used to stand for the whole journey from a mine.
Crushing and grinding make particles smaller. Concentration increases the proportion of valuable minerals in a stream. Smelting uses high temperatures and chemical reactions to separate metals from their feed. Refining further removes unwanted components. Finally, alloying deliberately adds other metals to achieve useful properties.
Plants combine these operations in different ways. A simplified diagram is a map of the main possibilities, not a working plant specification or a set of instructions for extracting metal at home.
- Lead-associated ores
- Concentration and smelting → silver-bearing lead → desilverizing and further refining.
- Copper-associated ores
- Copper production and electrorefining → anode slimes → precious-metal recovery and refining.
- Other suitable silver-bearing ores
- Preparation → a selected extraction route, which may include leaching → recovery and refining.
- Recycled silver-bearing material
- Sorting and sampling → treatment matched to the feed → refining and new products.
First, reduce the amount that must travel
Mining brings material to the surface, but much of its mass may have little value to the recovery process. Separating a concentrate can reduce the amount sent onward for treatment. In flotation, controlled differences in particle surfaces help selected minerals attach to bubbles and enter a concentrate.
The output is still not a bar of fine silver. It is an intermediate whose composition matters to the next operator. Material that does not enter the concentrate becomes another stream, often tailings, which still requires responsible management.
A collector can think of this as the first major change in scale: a geological body becomes a flow of selected materials, each with its own destination and records.
Read the source: Metso’s explanation of flotation.
Lead can collect silver, then be separated from it
Silver and lead have a long metallurgical relationship. In cupellation, a lead-rich metal containing silver is heated under oxidizing conditions. Lead is converted to an oxide and separated, leaving a precious-metal-rich remainder. Historical evidence for this route connects mine landscapes, furnaces and the production of money.
The later Parkes process uses zinc to help remove precious metals from molten lead. It is a different separation step, not another name for cupellation. The resulting silver-rich material still needs further treatment.
Keep the sequence clear: recovering silver into a richer intermediate, separating it from its carrier metal and refining it to a final specification are not interchangeable claims.
Read the source: Historical Metallurgy on cupellation.
Copper, gold and silver ores take other paths
In copper electrorefining, a copper anode dissolves while copper is deposited at a cathode. Valuable metals, including silver, can be recovered from the anode slimes. That residue is a feed for further recovery, not waste that can simply be discarded.
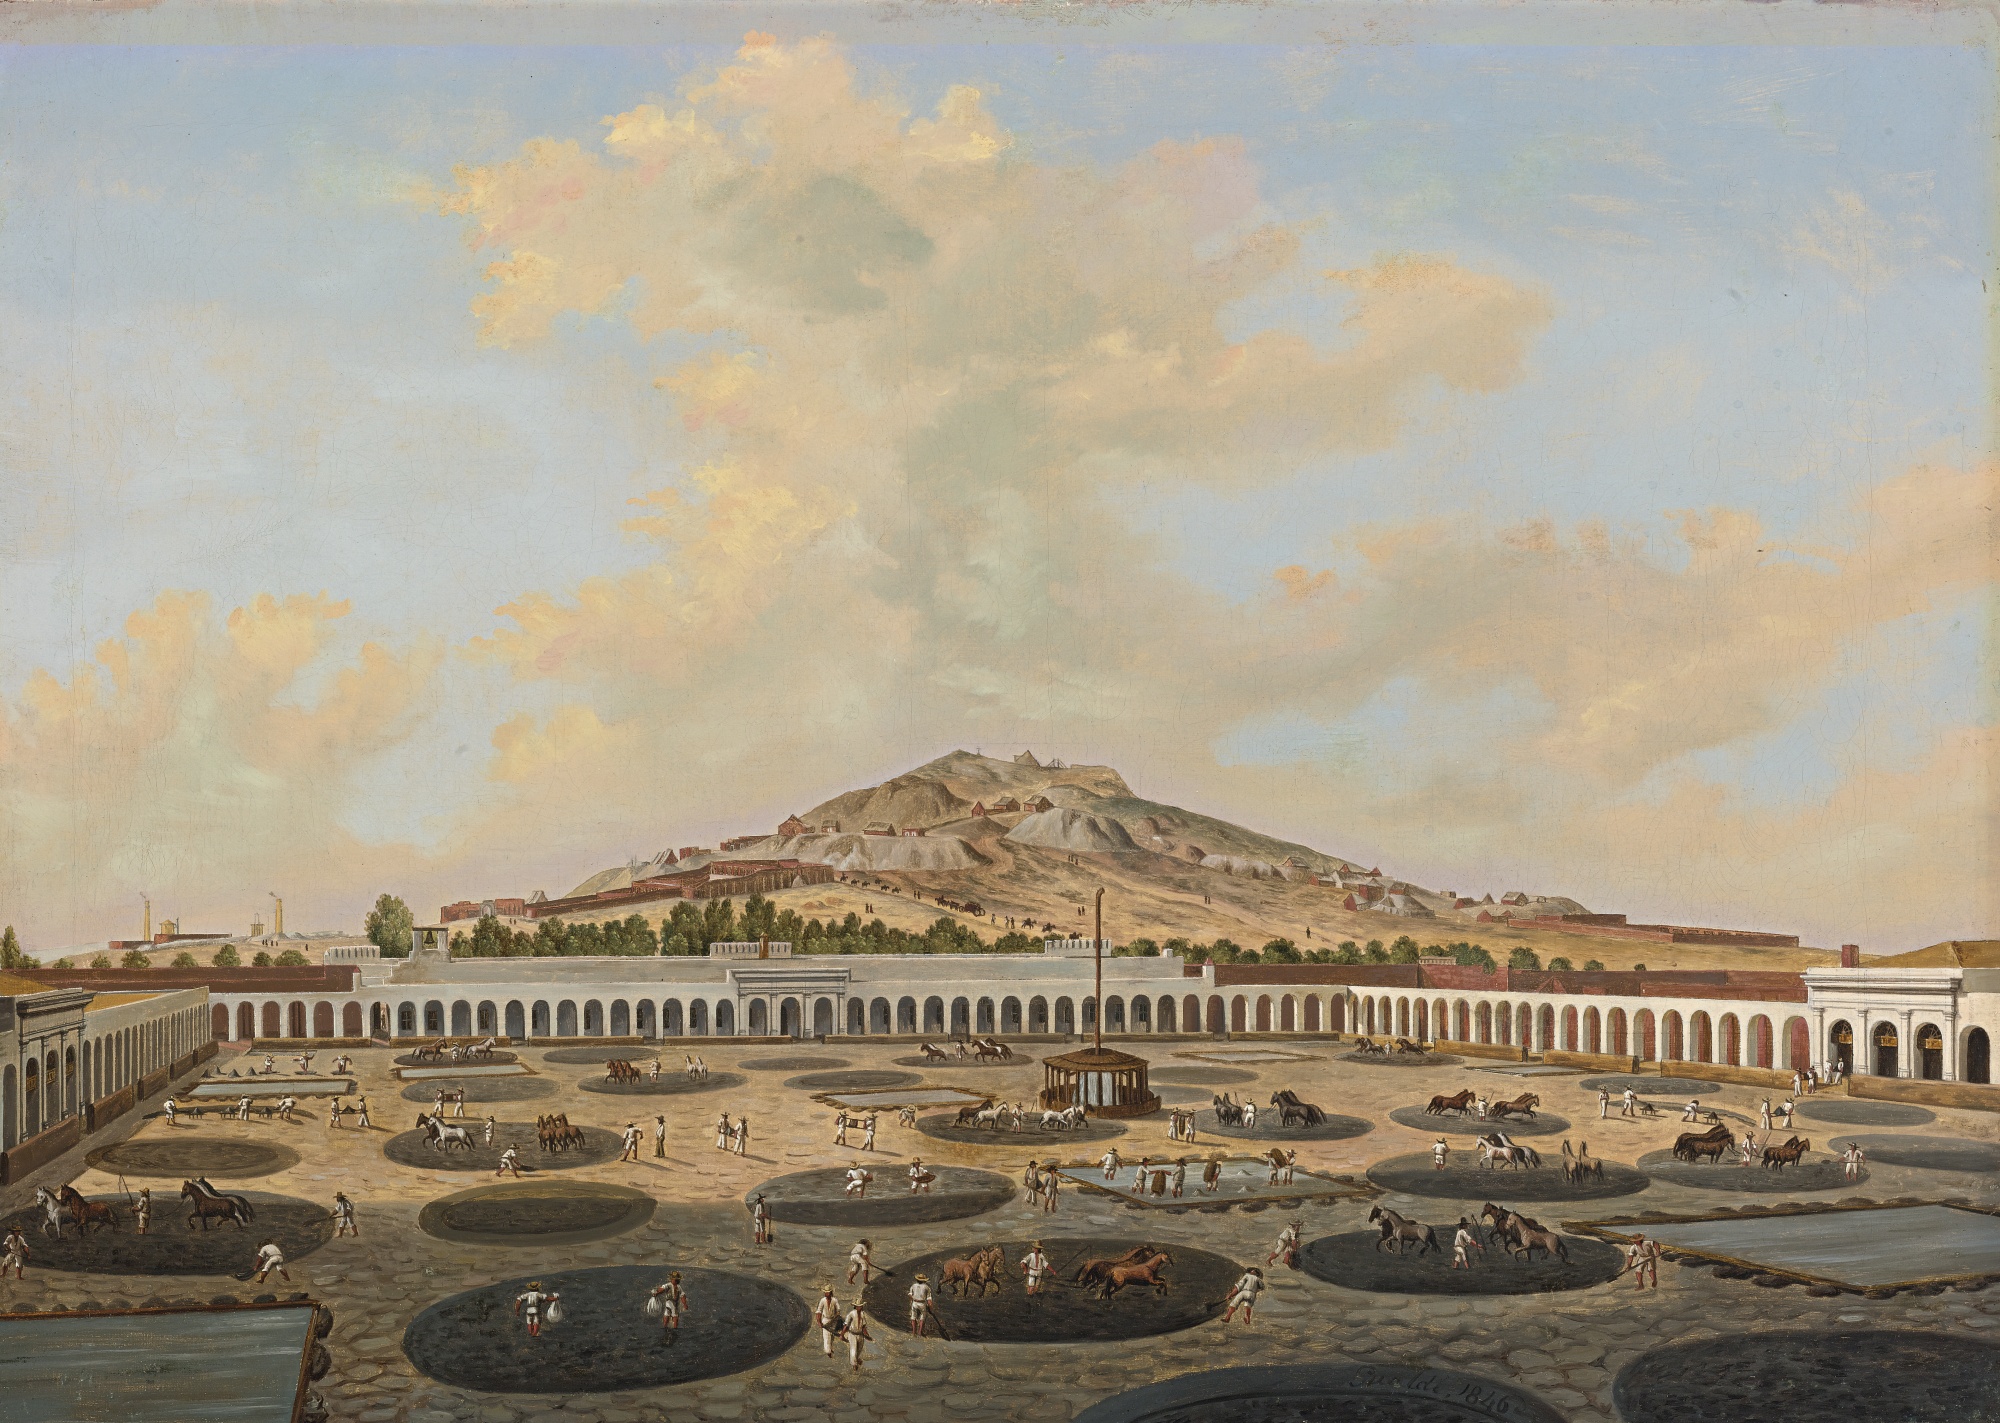
Other ores are treated by leaching: selected components pass into solution before recovery. Historical mercury amalgamation provided another route, particularly important in the colonial Americas. It left a very different technical and environmental legacy.
These are industrial and historical descriptions. Mercury and lead processes present serious hazards. A collector does not need to reproduce them to understand why different ores led to different technologies.
Read the source: Metso’s precious-metals recovery routes.

A sample must speak for the material
A refinery’s analytical result begins with a sampling decision. Mixed scrap, an intermediate bullion and a homogeneous silver alloy present different problems. A very precise measurement of an unrepresentative sample can still give a poor account of the lot. Ask what was sampled, how the sample represents the material and what the reported uncertainty covers.
An assay establishes composition within a method’s scope. ISO 11427:2024 describes potentiometric determination of silver in material considered homogeneous, preferably from 100 to 999 parts per thousand. Its abstract directs higher fineness toward a spectroscopic method by difference. ISO 15096:2020, confirmed in 2025, uses ICP-OES to determine impurities and derive silver content by difference; it recommends the method at 999 parts per thousand and above, with modifications at 999.9 and above.
Those are different analytical approaches, not a rule that one instrument can settle every question. A report needs a defined sample, a suitable method, calibration and a statement of what was measured. Neither an extra decimal place nor the word “certified” substitutes for that context.
Testing an object is a different question
X-ray fluorescence, or XRF, can provide useful elemental information without taking a conventional sample. The region contributing to the reading depends on the material, the instrument and the X-ray energies used. A coating or an altered surface can make the result differ from the bulk beneath it. There is no single penetration depth that describes every silver measurement.
Manufacturers also use XRF specifically to measure coatings. That application requires an appropriate model and calibration; it does not turn an ordinary spot reading into proof of a whole object’s construction. Hollow sections, fillers, soldered joints and composite layers deserve attention beyond the number on the screen.
For a collectible, establish what a test could change or damage before agreeing to it. See the authenticity guide for practical limits and the provenance guide for the separate question of origin.
Read the source: Hitachi High-Tech’s silver-coating XRF example.
From a refinery specification to mill stock
Electrolytic silver refining can move silver from an impure anode into a high-purity deposit. The recovered metal can then be melted and supplied in commercial forms. Refineries also handle secondary material, connecting newly mined supply with the recycling stream.
A specification has a defined scope. ASTM’s current B413-26 covers refined silver in cast-bar form. It should not be treated as a universal product specification for sheet, powder, paste or a finished jewel. A buyer may need limits on impurities as well as dimensions, mechanical condition or other application-specific requirements.
The next business may be an alloy producer, rolling mill, wire maker or chemical processor. It can turn specified silver into a deliberately chosen alloy or another working material. Read alloys and material forms for that handoff, then how makers shape silver for what happens next.
Read the source: Metso’s silver electrorefining example.
Look outside the furnace, too
Every route has material consequences beyond the recovered silver: energy demand, water use, air emissions, residues and the conditions of work. Their scale depends on the ore, process, site and management. A polished bar cannot tell you those facts on its own.
A stronger question than “Is silver sustainable?” is “What is known about this supply chain, and what evidence supports that claim?” The Potosí history shows why technology and labor must be read together. The provenance guide explains why certification and physical traceability also need to be distinguished.
Sources & further reading
Reviewed 11 November 2026. Institutional references support the history and process descriptions; standards apply only within their stated scope. Manufacturer sources document examples, not universal recipes. Photographs have individual source and rights records. This guide does not authenticate an object or certify its supply chain.
- USGS: silver statistics and information
- LBMA Responsible Silver Guidance, version 2
- Historical Metallurgy: silver refining and cupellation
- EPA: mineral processing sectors, including lead desilverization
- Metso: flotation and the separation of mineral particles
- Metso: precious metals recovery from anode slimes
- Metso: silver electrorefining
- ASTM B413-26: Standard Specification for Refined Silver (cast bars)
- ISO 11427:2024: determination of silver by potentiometry
- ISO 15096:2020: high-purity silver, difference method using ICP-OES
- Hitachi High-Tech: using XRF to control silver coating thickness
- Bruker: what determines XRF information depth